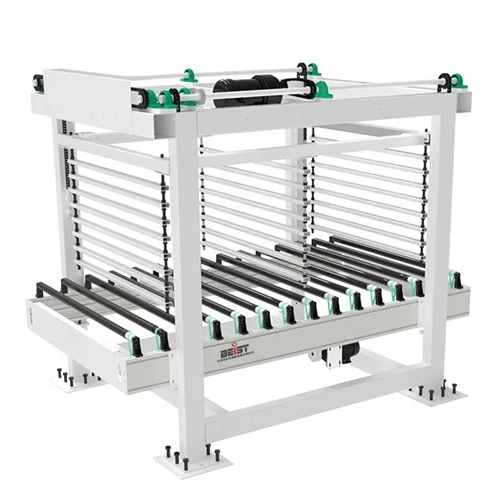
Sorting roller conveyors are a common sight in various industries, facilitating the efficient movement and organization of goods. As a leading supplier of sorting roller conveyors, one question that frequently arises is whether these conveyors can be effectively used for sorting pharmaceutical products. In this blog, we will explore the feasibility, advantages, and considerations of using sorting roller conveyors in the pharmaceutical industry.
Feasibility of Using Sorting Roller Conveyors for Pharmaceutical Products
The pharmaceutical industry has stringent requirements for product handling, storage, and transportation. These requirements are in place to ensure the safety, efficacy, and quality of pharmaceutical products. Sorting roller conveyors can be a viable solution for sorting pharmaceutical products, provided that they are designed and configured to meet these specific requirements.
One of the primary concerns in the pharmaceutical industry is the prevention of product contamination. Sorting roller conveyors can be constructed using materials that are compatible with pharmaceutical products, such as stainless steel or plastic. These materials are easy to clean and sanitize, reducing the risk of contamination. Additionally, the conveyors can be equipped with features such as enclosed frames and covers to further protect the products from dust, debris, and other contaminants.
Another important consideration is the accuracy and precision of sorting. Pharmaceutical products often come in various shapes, sizes, and weights, and they need to be sorted accurately to ensure proper packaging and distribution. Sorting roller conveyors can be equipped with advanced sensors and control systems to detect and sort products based on their size, weight, shape, or other characteristics. These systems can be programmed to sort products with high accuracy and precision, reducing the risk of errors and improving overall efficiency.
Advantages of Using Sorting Roller Conveyors in the Pharmaceutical Industry
There are several advantages to using sorting roller conveyors in the pharmaceutical industry. Some of these advantages include:

- Improved Efficiency: Sorting roller conveyors can significantly improve the efficiency of pharmaceutical product sorting processes. By automating the sorting process, these conveyors can reduce the time and labor required for manual sorting, allowing pharmaceutical companies to increase their production capacity and meet the growing demand for their products.
- Enhanced Quality Control: Sorting roller conveyors can help pharmaceutical companies maintain strict quality control standards. By accurately sorting products based on their characteristics, these conveyors can ensure that only high-quality products are packaged and distributed. This can help reduce the risk of product recalls and improve customer satisfaction.
- Flexibility: Sorting roller conveyors can be customized to meet the specific needs of pharmaceutical companies. They can be designed to handle different types of pharmaceutical products, including bottles, vials, blister packs, and cartons. Additionally, these conveyors can be integrated with other equipment, such as labeling machines, packaging machines, and barcode scanners, to create a complete sorting and packaging system.
- Cost Savings: Sorting roller conveyors can help pharmaceutical companies save costs in the long run. By reducing the time and labor required for manual sorting, these conveyors can lower the overall production costs. Additionally, by improving the efficiency and quality of the sorting process, these conveyors can help reduce the risk of product waste and rework, further saving costs.
Considerations for Using Sorting Roller Conveyors in the Pharmaceutical Industry
While sorting roller conveyors can offer several advantages for the pharmaceutical industry, there are also some considerations that need to be taken into account. Some of these considerations include:

- Regulatory Compliance: The pharmaceutical industry is highly regulated, and companies need to ensure that their sorting roller conveyors comply with all relevant regulations and standards. This includes regulations related to product safety, quality control, and environmental protection. Pharmaceutical companies should work closely with their sorting roller conveyor suppliers to ensure that the conveyors are designed and configured to meet these requirements.
- Cleaning and Sanitization: As mentioned earlier, the prevention of product contamination is a critical concern in the pharmaceutical industry. Sorting roller conveyors need to be cleaned and sanitized regularly to ensure that they are free from dust, debris, and other contaminants. Pharmaceutical companies should establish a comprehensive cleaning and sanitization protocol for their sorting roller conveyors and ensure that all employees are trained on how to follow these procedures.
- Maintenance and Repair: Sorting roller conveyors are complex pieces of equipment that require regular maintenance and repair to ensure their optimal performance. Pharmaceutical companies should establish a maintenance schedule for their sorting roller conveyors and ensure that all maintenance and repair tasks are carried out by qualified technicians. Additionally, companies should keep spare parts on hand to minimize downtime in the event of a breakdown.
- Integration with Existing Systems: Pharmaceutical companies often have existing production and packaging systems in place. When implementing a sorting roller conveyor, it is important to ensure that it can be integrated seamlessly with these existing systems. This may require the use of specialized interfaces and control systems to ensure that the conveyor can communicate effectively with other equipment.
Types of Sorting Roller Conveyors Suitable for Pharmaceutical Products
There are several types of sorting roller conveyors that are suitable for sorting pharmaceutical products. Some of these types include:
- Gravity Skate Wheel Conveyor: Gravity skate wheel conveyors are a popular choice for sorting pharmaceutical products. These conveyors use a series of skate wheels to move products along the conveyor. They are ideal for handling lightweight products and can be easily customized to meet the specific needs of pharmaceutical companies.
- Gravity Roller Conveyor: Gravity roller conveyors are another common type of sorting roller conveyor used in the pharmaceutical industry. These conveyors use a series of rollers to move products along the conveyor. They are suitable for handling heavier products and can be designed to accommodate different types of pharmaceutical products.
- Curved Roller Conveyor: Curved roller conveyors are used to change the direction of product flow. They are often used in pharmaceutical production and packaging lines to create a more efficient layout. Curved roller conveyors can be customized to meet the specific needs of pharmaceutical companies and can be designed to handle different types of pharmaceutical products.
Conclusion
In conclusion, sorting roller conveyors can be a viable solution for sorting pharmaceutical products. They offer several advantages, including improved efficiency, enhanced quality control, flexibility, and cost savings. However, there are also some considerations that need to be taken into account, such as regulatory compliance, cleaning and sanitization, maintenance and repair, and integration with existing systems. By working closely with a reputable sorting roller conveyor supplier, pharmaceutical companies can ensure that they select the right conveyor for their specific needs and that it is designed and configured to meet all relevant regulations and standards.

If you are a pharmaceutical company looking for a reliable sorting roller conveyor solution, we encourage you to contact us. Our team of experts can help you select the right conveyor for your specific needs and provide you with a customized solution that meets all your requirements. We look forward to the opportunity to work with you and help you improve the efficiency and quality of your pharmaceutical product sorting processes.
References
- [Title of Book 1], Author 1, Publisher 1, Year 1
- [Title of Journal Article 1], Author 2, Journal Name 1, Volume 1, Issue 1, Pages 1 - 10, Year 2
- [Title of Industry Report 1], Organization 1, Year 3